Quiet Operation
Internal drive eliminates chain and belt noise — critical for distribution centers, food processing, and pharmaceutical applications where noise levels matter.
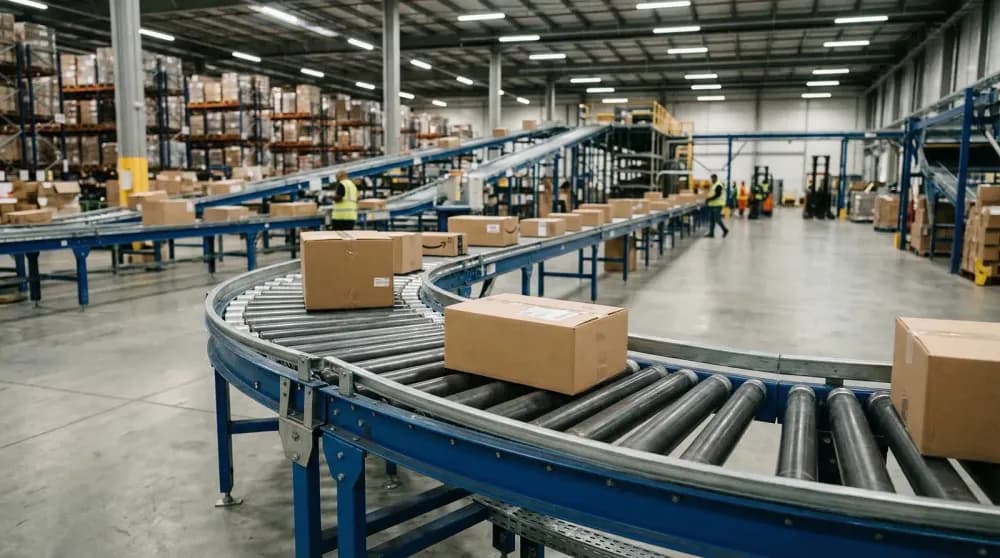
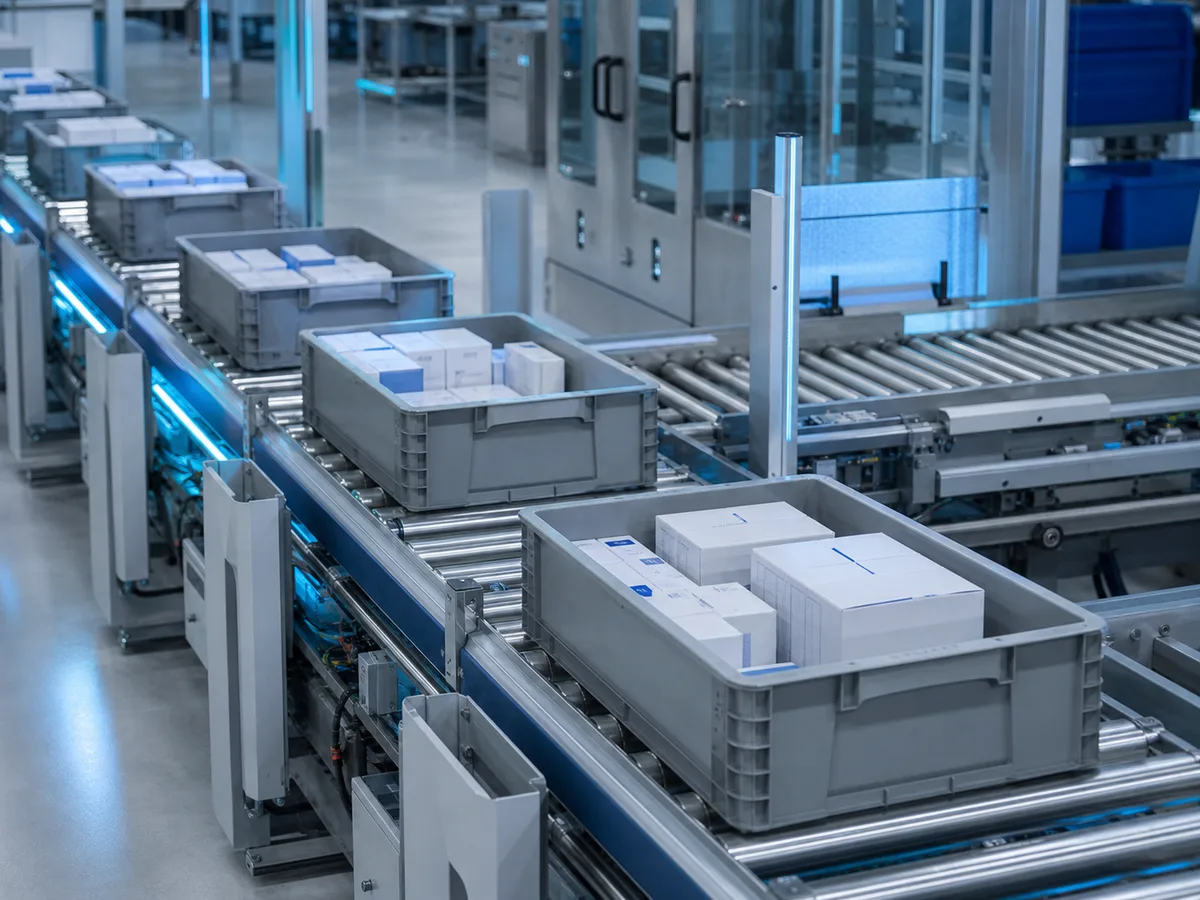
Motorized conveyor rollers integrate the drive system inside the roller tube, eliminating external motors, gearboxes, chains, and belts. The result is a quieter, cleaner, more energy-efficient conveyor system that's simpler to install and maintain. TelcoMotion engineers motorized rollers to your conveyor's specific load, speed, and zone-control requirements — not selected from a generic catalog.
Internal drive eliminates chain and belt noise — critical for distribution centers, food processing, and pharmaceutical applications where noise levels matter.
Zero-pressure accumulation with individual zone control means rollers only run when product is present — reducing energy consumption 50–70% versus conventional belt conveyors.
No external chains, belts, or sprockets to adjust, lubricate, or replace. Roller replacement in under 5 minutes without tools in most configurations.
Standard ranges are starting points. Every TelcoMotion motor is designed to your application's exact requirements.
TelcoMotion motorized rollers are specified for your conveyor's zone length, product weight, speed profile, and control architecture. We engineer the motor winding, gear ratio, and tube configuration together — optimizing for your throughput requirement and providing full zone-control integration support.
Request a Specification →Share your requirements — our engineering team responds within 48 hours with a configuration assessment.